About Industrial Storage
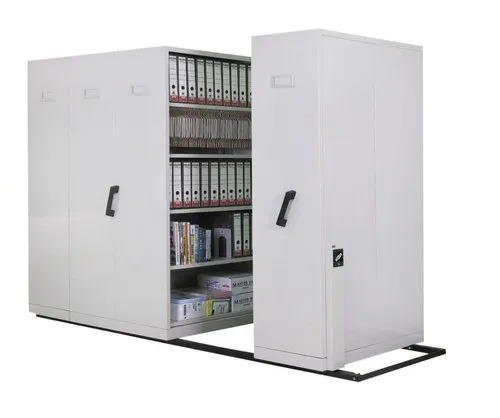
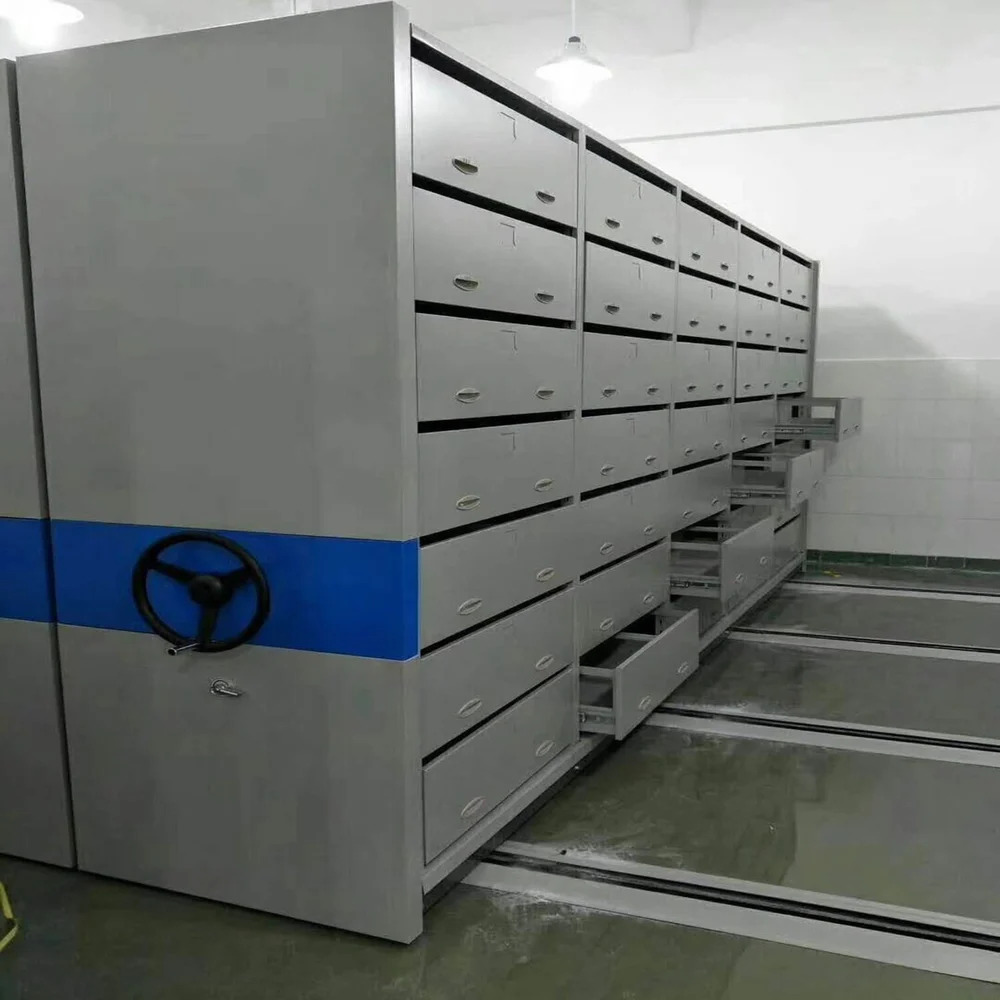
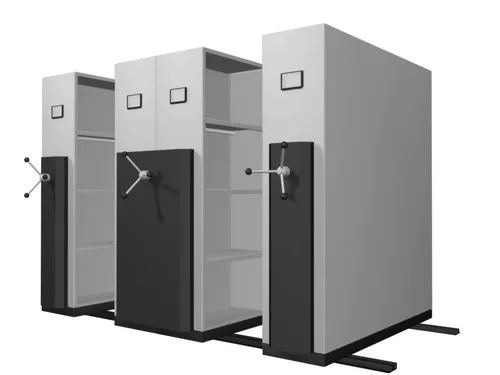
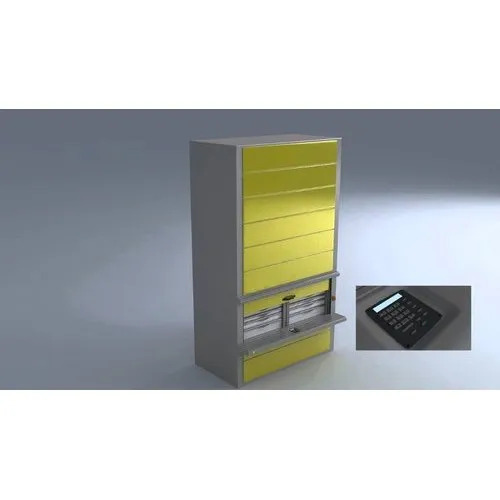
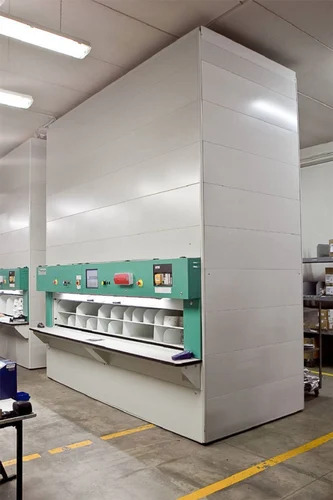
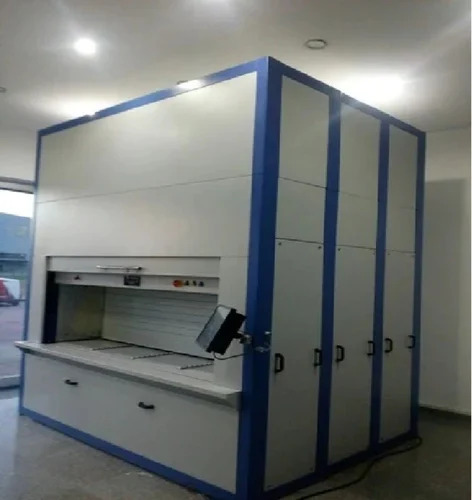
Experience our Exquisite Industrial Storage Solution, renowned as a hot-selling and meritorious choice for evolving storage demands. With a robust mechanical operation, this reduced-maintenance, powder-coated mobile compactor delivers outstanding load capacity per bay (300-600 kg), accommodating more than eight shelves and seven swift-access levels. Limited stock available of this premium, best-in-class system, finished in crisp white mild steel. Designed for installations above 10 ft in height and over 12,000 mm in length, with secure handle-locking and easy floor-rail mobility, it is ideal for every industrial need. Manufactured and supplied across India-order now!
Industrial Storage for Broad Plant Applications
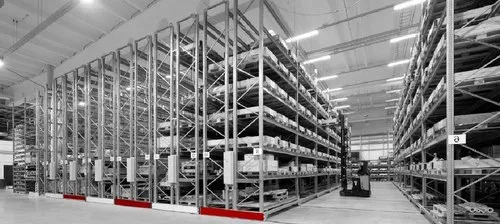
Our mechanical mobile compactor storage is extensively deployed across manufacturing plants, warehouses, factories, and processing units. Designed for a variety of industrial sectors, it is regularly used by operations managers, facility supervisors, and logistics coordinators. The high load and multi-level shelving support efficient inventory management and space optimization, making it an ideal fit for production lines or storage zones demanding robust, readily accessible storage solutions.
Export Markets, Certifications, and Supply Terms
Our industrial storage units cater to major export markets in Asia, Africa, and the Middle East. Each system adheres to national and international quality certifications, ensuring reliability and compliance. Proposal amounts and asking prices are available upon request, and transportation arrangements are efficiently coordinated for timely delivery. With strong supply ability, we handle bulk orders while meeting stringent export requirements, providing clients with certified excellence and seamless logistics support worldwide.
FAQ's of Industrial Storage:
Q: How does the mobile compactor system operate mechanically?
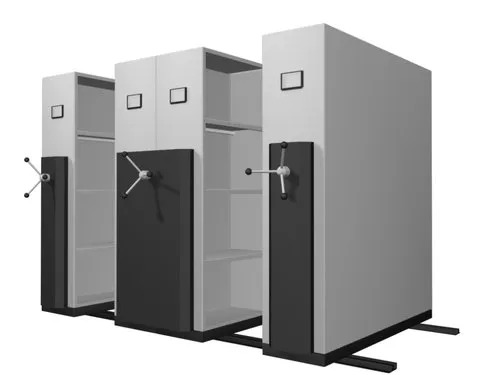
A: The mobile compactor operates with a manual handle mechanism, moving the shelves smoothly on floor rails for easy access and optimized space utilization without requiring electrical power.
Q: What benefits does this industrial storage unit offer?
A: It provides a robust structure with high load capacity, maximizing storage efficiency. Its exquisite finish and secure locking system ensure both safety and longevity, making it suitable for intensive industrial environments.
Q: Where can these storage systems be installed?
A: These storage units are ideal for installation in industrial plants, warehouses, factories, and any facility requiring efficient, high-volume storage for heavy or bulk items.
Q: What is the process for ordering and delivery?
A: Interested buyers can request a proposal amount and negotiate the asking price. Transportation and installation will be arranged once the order is confirmed, ensuring reliable supply and prompt setup across India and export markets.
Q: How many shelves and levels are included in the unit?
A: The storage system features more than eight shelves distributed across seven levels, allowing for a flexible arrangement of items according to weight and size requirements.




 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
 Send Inquiry

 Send Inquiry


